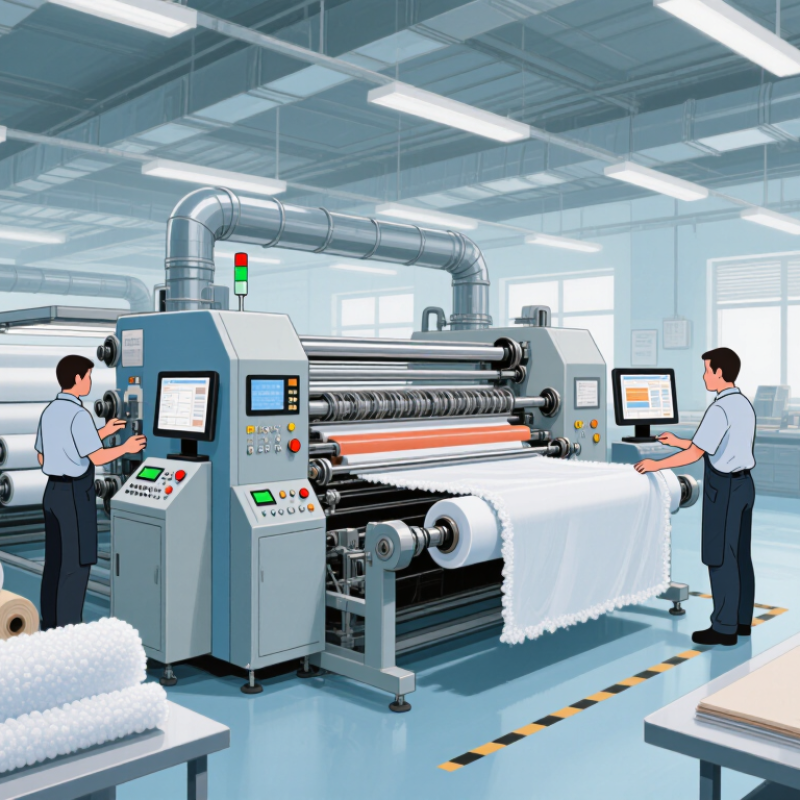
| 1 | Hot-Melt Roll-to-Roll Laminator | Applies thermoplastic adhesive film or web between textile layers using heated rollers and controlled nip pressure. | Polyester, nylon, cotton blends, nonwovens, foam, membrane fabrics, and synthetic leather. | 1,600–3,200 mm | 60–180°C; 5–40 m/min | Continuous production with uniform adhesive coating and stable web tension. | ISO 12947 Can produce consistent multilayer constructions for abrasion testing. ASTM D751 Useful for coated-fabric specimens when the laminate includes a coated substrate. |
| 2 | Flame Lamination Machine | Uses controlled flame to activate the surface of polyurethane foam before pressing it against a textile layer. | Upholstery fabric, automotive textiles, foam-backed fabric, mattress textiles, and acoustic materials. | 1,600–2,800 mm | Flame intensity controlled by gas flow; 5–30 m/min | High-throughput foam-to-fabric bonding without a separate liquid adhesive coating station. | EN 13501-1 The final laminate must be fire-classified as a complete construction; the machine itself does not provide a fire rating. ISO 12947 Supports preparation of bonded textile samples for durability evaluation. |
| 3 | Powder-Dot Adhesive Laminator | Deposits thermoplastic adhesive powder in a controlled dot pattern, then melts and bonds the layers through a heated calender or press. | Garment interlinings, technical textiles, breathable laminates, fleece, woven fabrics, and knit fabrics. | 1,600–2,400 mm | 100–160°C; 8–35 m/min | Adjustable adhesive add-on and dot density; helps preserve fabric softness and breathability. | ISO 12947 Useful where controlled adhesive distribution is required before Martindale abrasion testing. Fire performance under EN 13501-1 depends on all laminate components and the tested end-use assembly. |
| 4 | Hot-Air Laminator | Softens a thermoplastic film or adhesive web with heated air before combining textile layers in a pressure nip. | Outdoor fabrics, waterproof-breathable membranes, medical textiles, protective clothing, and sportswear. | 1,600–3,000 mm | 80–220°C; 3–25 m/min | Low-contact heating and adjustable air circulation for sensitive or dimensionally unstable fabrics. | ASTM D751 Suitable for manufacturing coated-fabric constructions that may be evaluated for adhesion, bursting strength, hydrostatic resistance, or related properties under the applicable method. Final compliance requires laboratory testing. |
| 5 | Thermal Calender Laminator | Combines layers through heated steel or elastomer-covered rollers with controlled temperature, pressure, and line speed. | Nonwovens, geotextiles, filtration media, decorative textiles, carpet backings, and multilayer technical fabrics. | 1,800–3,600 mm | 60–200°C; 5–50 m/min | High-speed bonding with precise nip control and good thickness uniformity across wide webs. | ISO 12947 Appropriate for laminates requiring repeatable thickness and surface construction before abrasion evaluation. EN 13501-1 Fire classification must be established using the finished product and its intended mounting arrangement. |
| 6 | Hot-Press Flatbed Laminator | Uses heated platens and controlled pressure to bond cut panels, small rolls, or layered fabric assemblies in batch operation. | Protective garments, upholstery panels, automotive interiors, composites, labels, and small-batch technical textiles. | 600–2,000 mm platen width | 80–200°C; 0.2–0.8 MPa; programmable dwell time | Batch production with accurate pressure and dwell-time control; suitable for sampling and product development. | ASTM D751 Convenient for producing controlled coated-fabric panels and laboratory samples. ISO 12947 Can support repeatable specimen preparation, but abrasion results must be obtained using the prescribed test apparatus and procedure. |
| 7 | Ultrasonic Textile Laminator | Uses high-frequency mechanical vibration to generate localized heat and bond thermoplastic layers without continuous external heating. | Nonwovens, hygiene fabrics, filtration media, protective clothing, medical textiles, and lightweight synthetic laminates. | 600–2,000 mm | 20–35 kHz; 2–20 m/min | Fast localized bonding with low adhesive use and limited heat exposure to surrounding fabric areas. | ISO 12947 Useful for developing lightweight bonded constructions for abrasion assessment. For EN 13501-1, flame classification applies to the completed textile assembly, including seams, coatings, adhesives, and backing materials. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS