| Web Width | Match the usable coating width; allow approximately 50–150 mm total edge margin. | The machine should accommodate the widest production web without excessive unused area or edge instability. The usable coating width is normally smaller than the maximum mechanical web width. | Confirm maximum web width, minimum web width, edge-margin requirements, and whether future products require wider tooling. |
| Coating Weight | Define the target in g/m² and specify the acceptable tolerance, commonly within approximately ±3–5% of the setpoint. | Coat weight affects bond strength, release performance, drying load, material consumption, and final product thickness. | Use gravimetric measurement: weigh a known coated area, remove the adhesive, reweigh, and calculate dry or wet coat weight as required. |
| Cross-Web Uniformity | ±3–5% target | Uniform coating across the web reduces weak-bond areas, adhesive squeeze-out, blocking, curl, and variation in downstream converting. | Measure multiple locations across the web, including both edges and the center, under stable production conditions. |
| Machine Speed | Select a rated speed above the required production speed, with practical allowance for adhesive type and drying capacity. | Higher line speed can reduce residence time, making metering stability, web handling, and drying performance more demanding. | Request a trial at the intended substrate, coat weight, adhesive viscosity, and target production speed. |
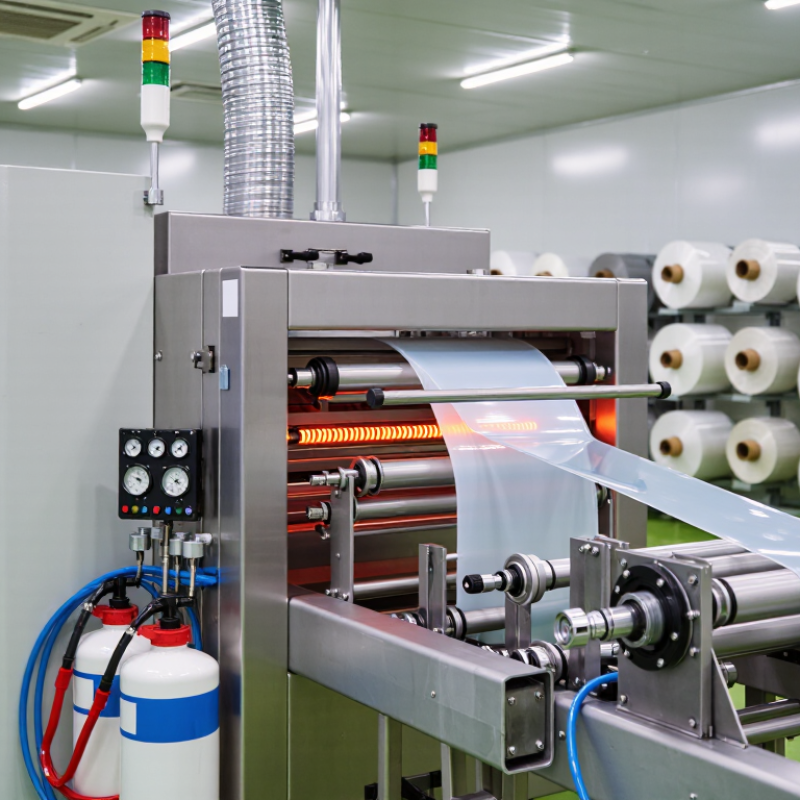
| Coating Method | Choose gravure, reverse-roll, slot-die, knife, or another method according to coat-weight range and product tolerance. | Gravure and reverse-roll systems are commonly used for controlled thin coatings; slot-die systems can provide precise, low-waste application when the fluid and process window are suitable. | Compare usable coat-weight range, setup time, cleaning requirements, speed capability, and sensitivity to adhesive rheology. |
| Adhesive Viscosity | Specify the operating viscosity range at the actual coating temperature. | Viscosity influences pump selection, flow stability, metering, coating defects, and the achievable coat-weight range. | Record viscosity with a defined test method and temperature; verify compatibility with pumps, hoses, filters, and coating hardware. |
| Adhesive Chemistry | Identify water-based, solvent-based, hot-melt, or UV/EB-curable adhesive requirements. | Each chemistry requires suitable temperature control, drying or curing, ventilation, materials of construction, and safety provisions. | Confirm operating temperature, solvent or water load, curing requirements, exhaust needs, and applicable workplace regulations. |
| Drying or Curing Capacity | Size the dryer or curing unit for adhesive solids, web speed, coating weight, and required residual solvent or moisture level. | Insufficient drying may cause blocking, odor, poor winding, and unstable bond performance; excessive heat can damage heat-sensitive films. | Check temperature zones, airflow, exhaust volume, residence time, and substrate temperature limits during a production-representative trial. |
| Web Tension Control | Use closed-loop tension control appropriate for the substrate and web width. | Stable tension helps prevent wrinkles, lateral movement, stretching, registration errors, and uneven coating caused by web flutter. | Review unwind, infeed, coating, drying, and rewind tension ranges, along with load-cell or dancer-control capability. |
| Substrate Compatibility | Define film, paper, foil, nonwoven, or laminate structure, including thickness and surface treatment. | Surface energy, porosity, stiffness, thickness, and heat sensitivity affect wetting, adhesion, web transport, and drying behavior. | Provide representative substrate samples and verify wetting, adhesion, curl, blocking, and dimensional stability. |
| Edge Control | Specify edge guides, edge-bead management, side dams, and trim or masking requirements. | Controlled edges improve product yield and prevent adhesive buildup on rollers, dryers, and downstream slitting equipment. | Inspect edge profile at the target speed and coat weight; evaluate startup, shutdown, and splice behavior. |
| Process Measurement | Include flow, pressure, temperature, speed, tension, and coat-weight monitoring. | Real-time measurements help detect drift before it creates a large quantity of nonconforming material. | Confirm sensor accuracy, calibration intervals, alarm limits, data logging, and access to production trends. |
| Cleaning and Changeover | Specify cleaning time, solvent or water handling, removable components, and product-change frequency. | Fast, repeatable changeovers reduce downtime and lower the risk of dried adhesive, contamination, and coating defects. | Run a changeover demonstration using the actual adhesive family and review waste, flushing, access, and operator safety. |
| Quality Acceptance Criteria | Document web width, coat weight, cross-web uniformity, defects, adhesion, drying, and winding requirements. | Clear acceptance criteria prevent performance claims from being based only on maximum machine speed or nominal specifications. | Use a signed factory or site acceptance test based on representative materials and the agreed operating window. |
| Practical specification note: Treat the values above as starting points for equipment selection. Final limits should be confirmed through trials using the actual adhesive, substrate, web width, coat-weight range, production speed, and required product performance. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS