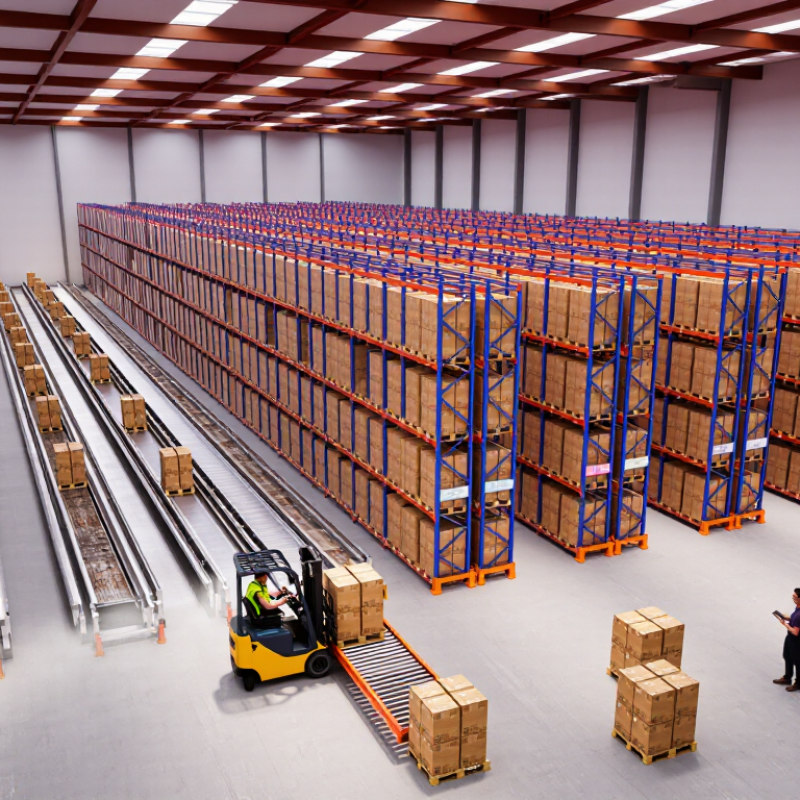
| Inventory Rotation | FIFO is the standard operating principle; suitable for products with expiry dates, batch control, or frequent replenishment. | Gravity lanes move older pallets toward the picking face first when loading and unloading rules are followed. | Choose pallet flow when stock rotation and controlled product sequencing are more important than maximum selectivity. | Define lot, batch, expiry, and replenishment rules before rack layout approval. |
| Pallet Compatibility | Confirm pallet length, width, bottom-board arrangement, rigidity, load condition, and allowable dimensional variation. | Roller tracks require stable pallet runners and a load base that can travel without snagging or tipping. | Use a dedicated lane configuration if pallet types cannot safely share the same track and brake settings. | Test representative empty and loaded pallets, including damaged or partially wrapped units. |
| Pallet Load | Specify the maximum gross pallet mass, load height, center of gravity, and load overhang rather than using an average weight. | Rack beams, frames, rollers, brakes, and stops must be selected for the actual operating load and impact conditions. | Size the system using the heaviest credible pallet and the most demanding handling condition. | Record load data on rack signage and verify that the design load matches the engineering calculations. |
| Lane Depth | Common applications use several pallet positions in depth; the appropriate depth depends on demand, replenishment frequency, and available building space. | Deeper lanes improve storage density but increase replenishment travel, load pressure, and the effect of pallet variation. | Use deeper lanes for high-volume, low-SKU operations and shorter lanes where access frequency or SKU variety is high. | Model inventory by SKU, daily pallet movement, lane occupancy, and replenishment windows. |
| SKU Profile | Best suited to multiple pallets per SKU or product families with predictable, repetitive demand. | A lane normally represents one SKU or a tightly controlled product group, which can reduce selectivity for slow-moving items. | Combine pallet flow with selective or other rack types when the operation carries many low-volume SKUs. | Calculate pallets per SKU, peak inventory, stock days, and the required number of active lanes. |
| Throughput and Handling | Evaluate pallet receipts, dispatches, peak-hour movements, forklift travel, and replenishment activity together. | A dense rack layout does not automatically increase throughput if aisles, docks, staging areas, or forklifts become bottlenecks. | Prioritize the complete material-flow path rather than storage capacity alone. | Validate travel paths, turning clearances, staging capacity, and peak-period congestion using a process simulation or time study. |
| Roller and Brake Configuration | Track pitch, roller diameter, lane slope, guide rails, speed controllers, and pallet separators must match the load characteristics. | Incorrect resistance or speed control can cause pallet collisions, unstable movement, or incomplete travel to the picking face. | Specify braking and separation components using tested load conditions, not nominal pallet weight alone. | Perform loaded travel tests at the first installed lane and confirm smooth movement at minimum and maximum loads. |
| Building Constraints | Review clear height, floor capacity, column spacing, sprinkler clearance, fire exits, dock positions, and emergency access. | Rack geometry must fit the building and comply with local fire, structural, and workplace safety requirements. | Approve the layout only after structural, fire-protection, and operational constraints have been checked. | Obtain a site survey and coordinate the final design with qualified structural and fire-safety professionals. |
| Safety and Compliance | Apply the current legal requirements and recognized rack-safety practices applicable to the installation location. | Pallet flow systems are exposed to forklift impact, moving loads, rack deflection, and component wear. | Include guards, end stops, back stops, load notices, pedestrian controls, and inspection procedures in the design. | Establish pre-use checks, documented inspections, damage reporting, quarantine procedures, and repair authorization. |
| Automation Readiness | Consider barcode or RFID identification, warehouse-management-system locations, sensors, and automated pallet handling where volumes justify it. | Digital controls can improve traceability, but they do not correct poor pallet quality or unsuitable lane design. | Design clear location logic and data interfaces before adding automation. | Test receipt, put-away, replenishment, picking, exception, and inventory-adjustment transactions. |
| Total Cost of Ownership | Compare rack, rollers, brakes, installation, floor work, protection, inspections, repairs, training, and future reconfiguration costs. | The lowest purchase price may create higher operating costs if components wear quickly or the layout limits future growth. | Select the design with the best cost per usable pallet position and cost per handled pallet over its planned service life. | Use a lifecycle comparison covering capacity, labor, maintenance, downtime, and expansion scenarios. |
| Commissioning and Training | Complete installation checks, load testing, operating instructions, and user training before routine production use. | Correct operating behavior is essential for safe FIFO performance and for preventing pallet or rack damage. | Treat commissioning as a formal project phase with acceptance criteria and documented handover. | Verify rack plumb, anchors, beam positions, lane movement, stops, labels, protection, and operator competency. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS