Change Language
Call Us08045479132

How to Choose an Engine Compressor?

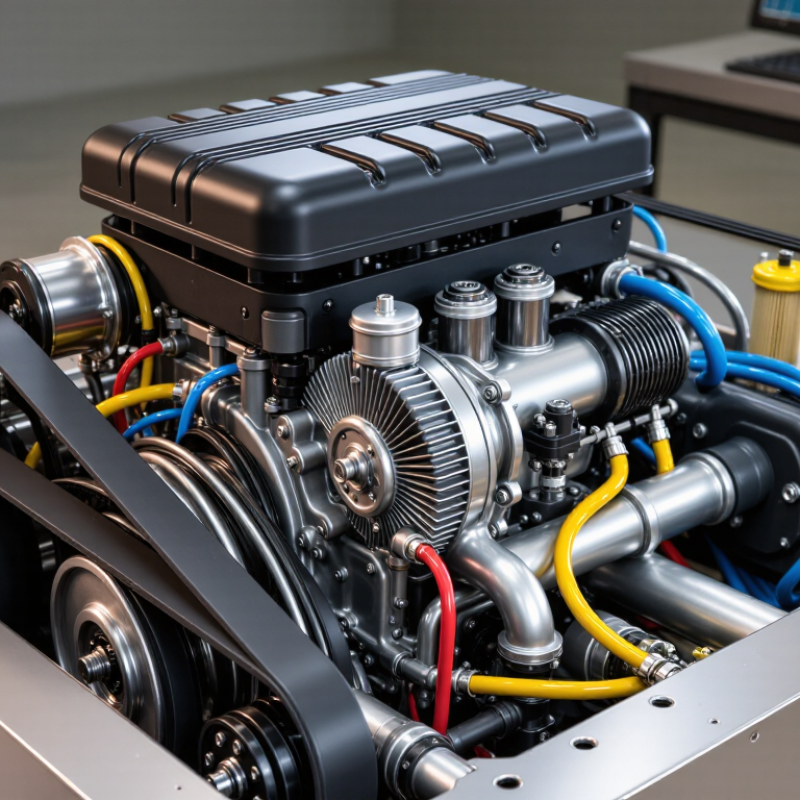
Choosing an Engine Compressor is not simply a matter of chasing the highest boost number. The right unit must match the engine’s displacement, operating speed, airflow demand, and intended duty cycle. A compressor used for a track car may face brief, aggressive loads. A commercial engine may run for hours near a steady speed. These conditions need different cooling, lubrication, and control strategies. Start with measured engine data, not a sales brochure. That distinction matters.

A practical selection process examines compressor map efficiency, pressure ratio, surge margin, temperature rise, and response time. It also checks mounting space, belt or exhaust compatibility, inlet filtration, and service access. For turbocharged systems, turbine matching affects compressor performance. For mechanically driven units, pulley ratio and parasitic loss deserve equal attention. Field evaluations often reveal installations that perform well on a dyno but overheat in real traffic. Peak output alone can mislead. Look at repeatable performance.

Reliable decisions combine manufacturer data with independent testing, qualified engineering review, and the engine builder’s records. Verify ratings under comparable temperature, altitude, fuel, and duty conditions. Confirm materials, seals, bearings, noise limits, and applicable industry requirements before purchase. A compressor that fits on paper may fail after vibration, dust, or heat exposure. No method is perfect. Measurements can be incomplete, and manufacturer comparisons may use different test conditions. Be willing to revise the choice when evidence disagrees. This guide explains how to compare options and select an Engine Compressor with balanced performance, durability, efficiency, and maintainability.

How to Choose an Engine Compressor?

Define the Engine Compressor’s Purpose and Operating Conditions

Before choosing an engine compressor, define its exact purpose. Start with the job. Will it supply pneumatic tools, support engine starting, or maintain pressure in a control system? Each task demands a different flow rate, pressure range, and response time. A compressor selected only by its maximum pressure may perform poorly during continuous operation.

Record the engine’s operating conditions in realistic detail. Measure required airflow at the working pressure, not only at idle. Check ambient temperature, altitude, humidity, and available installation space. A hot engine bay can raise intake temperatures and reduce compressor efficiency. Dusty environments also require stronger filtration and easier maintenance access. Consider the duty cycle carefully. Intermittent use may tolerate a smaller unit, while constant demand requires stable cooling and durable bearings.

Match the compressor’s output curve with the engine’s actual demand. Confirm shaft speed, mounting loads, lubrication needs, and control response with qualified technical data. Allow practical margin, but avoid excessive capacity. Oversizing can increase heat, energy use, and unnecessary mechanical stress. That assumption can fail. Field experience shows that vibration and poor hose routing often cause earlier problems than pressure limits. I would also review startup behavior under cold conditions, because laboratory ratings may not reflect real service. Keep inspection points visible, and document pressure, temperature, and noise during commissioning. Small measurements reveal larger design mistakes.

Compare Compressor Types and Their Performance Characteristics

Choosing an engine compressor starts with duty cycle, not catalogue horsepower. Reciprocating compressors deliver high pressure from a compact package, but their pulsating flow demands stronger piping and maintenance. Rotary screw units provide steadier airflow and suit long operating hours. Centrifugal compressors offer high flow with low vibration, yet efficiency can fall sharply below their design range.

The U.S. Department of Energy reports that compressed-air systems may consume about 10% of industrial electricity, while leaks can waste 20–30% of compressor output. That makes part-load performance important.

A variable-speed rotary screw compressor can reduce unloading losses during changing demand, although savings depend on controls, pressure settings, and maintenance. Numbers vary.

For engine applications, compare pressure ratio, mass flow, response time, discharge temperature, and adiabatic efficiency. Centrifugal designs respond quickly at high engine speed but may surge when airflow drops. Positive-displacement designs build boost earlier and tolerate wider operating conditions, though they can require more drive power.

ISO 1217 testing and ASME compressor performance methods help separate measured efficiency from optimistic sales estimates. Check the test conditions carefully. Field results are rarely identical. Record inlet temperature, altitude, filter restriction, and real load before choosing; a compressor that looks efficient on paper may perform poorly in a dusty, stop-start engine bay.

Match Capacity, Pressure Ratio, and Engine Requirements

Choosing an engine compressor starts with the engine, not the catalog. Define capacity as mass flow at actual inlet conditions. A compressor rated for 2,000 cubic meters per hour at sea level may deliver far less at altitude. Convert volume to mass flow before comparing equipment. The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks can waste 20–30% of compressor output. That loss can distort sizing.

Calculate pressure ratio with absolute pressures: discharge pressure divided by inlet pressure. Gauge pressure alone is misleading. An engine requiring 8 bar absolute from 1 bar absolute needs an 8:1 pressure ratio before piping losses. Check the compressor map at peak torque, rated speed, and acceleration. Keep the operating point away from surge and choke. Do not add an oversized safety margin automatically. It may reduce efficiency and response.

Match shaft power, speed range, cooling, lubrication, and control response to engine requirements. ISO 3046-1 requires engine power ratings to state reference conditions; high temperature and altitude can reduce available power. That interaction is often missed. In field checks, I verify filter loading, pipe losses, pressure pulsation, and fuel use during real duty cycles. A static test can look excellent. No map is perfect. Record inlet temperature, pressure, flow, and engine speed during commissioning. If results disagree, revisit the assumptions instead of forcing the compressor to fit.

Evaluate Efficiency, Materials, Controls, and Installation Constraints

Choosing an engine compressor starts with the duty cycle, not the catalogue horsepower. The U.S. Department of Energy reports that compressed-air systems may consume about 10% of industrial electricity. It also notes that leaks can waste 20–30% of compressor output. Therefore, compare specific power at the actual pressure, flow, and ambient temperature. A larger compressor may provide security, but part-load losses can erase that advantage. Ask for tested performance data, preferably under ISO 1217 conditions. Field measurements matter more than optimistic estimates.

Materials must match the gas, moisture, temperature, and operating environment. Stainless or coated components can reduce corrosion, but material upgrades do not fix poor filtration. For reciprocating units, inspect cylinder liners, valves, seals, and lubrication compatibility.

Controls deserve equal attention. Variable-speed control can reduce cycling, while sequencing multiple units may improve redundancy. The U.S. DOE’s Industrial Assessment Centers repeatedly identify pressure reduction, leak repair, and control optimization as practical energy-saving measures. Yet controls can become unstable when sensors are badly located. That mistake is easy to miss.

Tips: Measure inlet temperature, discharge pressure, flow, and fuel use for one full operating cycle. Leave service clearance around filters and coolers. Check foundation loading, ventilation, noise, and exhaust routing before purchase. A spreadsheet can still mislead. Recheck its assumptions with operating technicians. Installation constraints often decide whether a theoretically efficient compressor performs well in reality. Use documented test results, maintenance records, and a commissioning plan to support reliable decisions.

Check Reliability, Maintenance Needs, Cost, and Supplier Support

How to Choose an Engine Compressor?

Reliability should be checked beyond a polished product sheet. Ask for service records, operating hours, failure data, and performance tests from comparable applications. During inspection, listen for uneven vibration and check oil temperature after the compressor reaches working pressure. Small warning signs matter.

Maintenance needs often decide the real operating cost. Confirm filter intervals, seal replacement procedures, inspection access, and required tools. A compressor that needs frequent disassembly can interrupt production. Request a clear maintenance schedule with labor estimates. Be careful here. Suppliers may describe ideal conditions, not dusty workshops or heavy daily use.

Compare the purchase price with energy consumption, spare parts, downtime, and technician fees. A lower quote can become expensive after repeated repairs. Ask the supplier about parts availability, response times, training, and emergency support. Written service commitments are more useful than friendly promises. Check references from users with similar loads and climates. However, one reference is never enough. Operating habits differ, and even reliable equipment can perform poorly when installation is rushed. Keep room for that uncomfortable possibility. Choose the supplier who explains limitations openly and provides practical documentation, not only confident sales language.

How to Choose an Engine Compressor? - Check Reliability, Maintenance Needs, Cost, and Supplier Support

Compressor Type Typical Application Typical Discharge Pressure Capacity Range Reliability Profile Maintenance Needs Relative Purchase Cost Supplier Support Requirements Best Selection Scenario
Reciprocating High-pressure gas compression, pipeline service, gas gathering, and intermittent-duty applications Approximately 10–350 bar, depending on the number of stages and design Low to medium flow; commonly below 10,000 m³/h per unit Very high when correctly sized and operated; suitable for demanding pressure ratios High. Regular inspection of valves, piston rings, packing, lubrication, and vibration is required Medium to high Fast access to wearing parts, field technicians, overhaul capability, and application engineering When high pressure, strong turndown, and proven long-term serviceability are priorities
Rotary Screw Continuous-duty compressed air, process gas, and medium-pressure industrial systems Approximately 5–30 bar for common industrial configurations Medium to high flow; commonly 100–10,000 m³/h per unit High for continuous operation, provided oil quality, cooling, and filtration are controlled Medium. Oil, filters, separators, belts or couplings, and air-end condition require scheduled attention Medium Routine-service training, lubricant availability, controller support, and rapid replacement of consumables When steady flow, compact installation, and relatively simple operation are required
Centrifugal Large-volume process gas, utility air, refrigeration, and continuous-flow facilities Approximately 3–30 bar per casing; higher pressure may require multiple stages High to very high flow; commonly above 10,000 m³/h per unit High in stable operating conditions; surge, fouling, and rapid load changes must be managed Low to medium routine maintenance, but condition monitoring and specialist inspections are important High 24/7 technical response, surge-control expertise, balancing services, and planned major-overhaul support When very high flow, low vibration, and efficient continuous operation justify the investment
Rotary Vane Vacuum service, light industrial air systems, packaging, and material-handling equipment Typically up to approximately 10 bar in compression service; vacuum ratings vary by design Low to medium flow; commonly below 2,000 m³/h per unit Good for clean, moderate-duty applications; contamination and overheating can shorten service life Medium to high. Vanes, filters, seals, and lubricants may need frequent replacement in harsh service Low to medium Availability of vane kits, seals, filters, troubleshooting guidance, and local repair capability When the system needs a compact, economical solution for modest pressure or vacuum duties
Scroll Small clean-air systems, laboratories, medical equipment, and low-noise installations Typically 7–10 bar for standard compressed-air packages Low flow; commonly below 500 m³/h per unit High in clean, low-to-medium duty cycles; not generally intended for heavy continuous industrial loads Low routine maintenance, although air filters, cooling passages, and scroll elements must be monitored Low to medium Clear installation guidance, replacement-module availability, electrical support, and warranty service When low noise, oil-free air, compact size, and limited maintenance are more important than high capacity
Selection Note: Actual pressure, flow, efficiency, service interval, and total cost depend on gas composition, inlet conditions, duty cycle, engine speed, altitude, ambient temperature, control method, and required compression ratio. Compare complete life-cycle cost rather than purchase price alone.
Back to top