Profile A
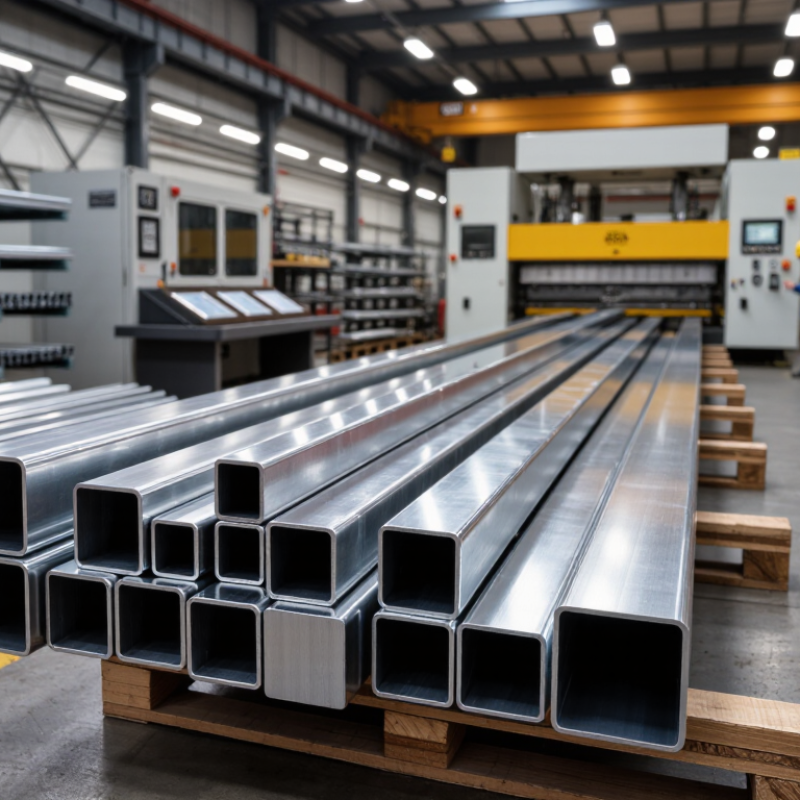
Structural Welded Tube Supplier | Carbon-steel square hollow sections commonly produced from approximately 20 × 20 mm to 400 × 400 mm, with wall thicknesses of about 1.5–20 mm. | S235 S355 ASTM A500 Grade B/C | Confirm outside dimensions, wall thickness, length tolerance, cutting method, bundle quantity, surface condition, and whether standard or custom sizes are required. | Check chemical composition, yield strength, tensile strength, elongation, dimensional tolerances, weld integrity, straightness, and visual surface quality. Require batch-based inspection rather than relying only on a sample. | Mill test certificate, dimensional inspection report, chemical analysis, mechanical test results, packing list, commercial invoice, and certificate of origin. | Usually 3–8 weeks after confirmation of specifications and receipt of the agreed payment, depending on production quantity and tooling requirements. | Compare full-container and consolidated cargo options. Protect bundles with steel straps, spacers, waterproof wrapping, and suitable container blocking to prevent movement and corrosion. |
Profile B
Precision Cold-Formed Tube Supplier | Light- to medium-wall square tubes for machinery, furniture, frames, and general fabrication. Frequently available from approximately 10 × 10 mm to 200 × 200 mm. | Low-carbon steel S235JR ASTM A513 | Specify corner radius, outer-dimension tolerance, wall-thickness tolerance, cut length, burr limits, end squareness, and required surface finish before placing the order. | Verify gauge calibration, corner radius, wall uniformity, tube straightness, weld-bead condition, end condition, and sampling frequency. Request first-article approval for non-standard profiles. | Product specification sheet, inspection plan, calibration records, material certificate, dimensional report, and pre-shipment inspection photographs. | Commonly 2–6 weeks for standard sizes; custom tooling or special tolerances may extend the schedule. | Smaller tubes can be nested to improve container utilization. Confirm maximum bundle weight, moisture protection, labeling, and unloading requirements at the destination. |
Profile C
Galvanized Square Tube Supplier | Pre-galvanized or hot-dip-galvanized square tubes for outdoor structures, fencing, agricultural equipment, and light construction applications. | Carbon steel S235/S275 ASTM A500 Zinc coating options | Define whether galvanizing is applied before or after forming, target zinc coating mass, tube dimensions, cut lengths, hole requirements, and acceptable coating appearance. | Measure zinc coating thickness or mass, inspect bare spots and runs, check adhesion and drainage holes where applicable, and verify steel dimensions after coating. Coating acceptance criteria should be agreed in writing. | Steel mill certificate, galvanizing certificate, coating test results, dimensional inspection report, packing list, and photos of bundle protection. | Generally 4–9 weeks, depending on whether galvanizing is performed in-line, after fabrication, or through an external processing facility. | Use dry, ventilated storage and avoid trapped moisture between tightly packed galvanized tubes. Confirm tariff classification, import duties, and destination-country corrosion requirements. |
Profile D
Stainless-Steel Tube Supplier | Decorative, sanitary, architectural, and process-grade square tubes, commonly supplied in sizes from approximately 10 × 10 mm to 300 × 300 mm. | 304/304L 316/316L EN 1.4301 EN 1.4404 | State grade, finish, surface protection film, weld condition, annealing requirements, length tolerance, corner radius, and whether the tube is intended for structural or hygienic use. | Confirm alloy composition through PMI or laboratory testing, inspect surface finish, check weld penetration, passivation condition, dimensional accuracy, and contamination control. | EN 10204 3.1 certificate or equivalent, PMI report, surface-finish report, dimensional inspection report, and packing declaration. | Typically 5–10 weeks because stainless production, finishing, and testing may require additional stages. | Separate stainless products from carbon-steel cargo to reduce iron contamination. Use protective film, clean packing materials, and dry container conditions. |
Profile E
Large-Section Structural Tube Supplier | Heavy square hollow sections for columns, bridges, industrial frames, and engineered structures, often exceeding 200 × 200 mm and requiring project-specific engineering review. | S355J2H ASTM A500 ASTM A1085 Project grades | Submit drawings, design loads, section dimensions, wall thickness, steel grade, impact-test temperature, weld requirements, end preparation, and permitted length range. | Use an approved inspection and test plan covering heat traceability, ultrasonic or other non-destructive testing where specified, weld quality, dimensional checks, and load-related documentation. | Material certificates, weld procedure records, NDT reports, inspection and test plan, heat-number traceability, test certificates, and final release note. | Often 6–14 weeks, with longer schedules possible for engineered sections, low-temperature impact testing, or project-specific documentation. | Check vessel weight limits, port lifting capacity, bundle length restrictions, cargo insurance, export packing rules, and delivery sequencing for construction sites. |
Profile F
Small-Batch Custom Tube Supplier | Custom dimensions, drilled or slotted sections, mitre cuts, welded assemblies, painted tubes, and mixed-size orders for prototypes or specialized projects. | Carbon steel Stainless steel Aluminum options Customer-specified grades | Provide CAD drawings, revision number, annual demand, trial quantity, packaging instructions, inspection points, and approval samples. Clarify minimum order quantities and setup charges. | Approve a golden sample, verify critical-to-function dimensions with a coordinate measuring machine where appropriate, inspect holes and cuts, and control drawing revisions throughout production. | Approved drawing, sample approval record, material certificate, dimensional report, surface-treatment certificate, final inspection report, and photographs. | Commonly 4–12 weeks, depending on programming, tooling, secondary processing, sample approval, and production volume. | Protect machined edges and finished surfaces individually. Consolidate compatible items, use moisture absorbers where needed, and mark each bundle against the packing list. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS