Change Language
Call Us08045479132

7 Tips for Choosing a Pneumatic Bending Machine?

Choosing a Pneumatic Bending Machine is not a simple matter of comparing prices. The right model must match material type, sheet thickness, bend angle, production volume, and available workshop space. A machine that performs well on thin aluminum may struggle with stainless steel or repeated sharp bends. In practical evaluations, operators should inspect frame rigidity, cylinder response, tooling alignment, and emergency stopping performance. Small details matter. Check air leaks. A pressure gauge that fluctuates during a test bend may indicate poor regulation or insufficient compressor capacity. Ask suppliers for documented specifications, test samples, maintenance guidance, and service response times. Independent certifications can support confidence, but they should never replace a hands-on inspection.

This guide presents seven practical tips for evaluating machine capability, control accuracy, safety features, operating costs, and supplier credibility. It also considers how easily technicians can change dies, clean the work area, and diagnose faults. Experienced buyers know that maximum force is only one part of the decision. Cycle consistency, noise, air consumption, and operator training often influence long-term value more strongly. Do not overlook ergonomics. A poorly positioned foot pedal or awkward loading height can create fatigue during a long shift. These recommendations reflect common fabrication needs and careful equipment comparison, not one brand’s sales language. Still, every workshop has different priorities. A careful buyer should record actual dimensions, sample results, and running costs before approval. No checklist is perfect. Test these tips against real jobs, real operators, and realistic production targets.

7 Tips for Choosing a Pneumatic Bending Machine?

Understanding Pneumatic Bending Machine Types and Applications

7 Tips for Choosing a Pneumatic Bending Machine?

Understanding Pneumatic Bending Machine Types and Applications

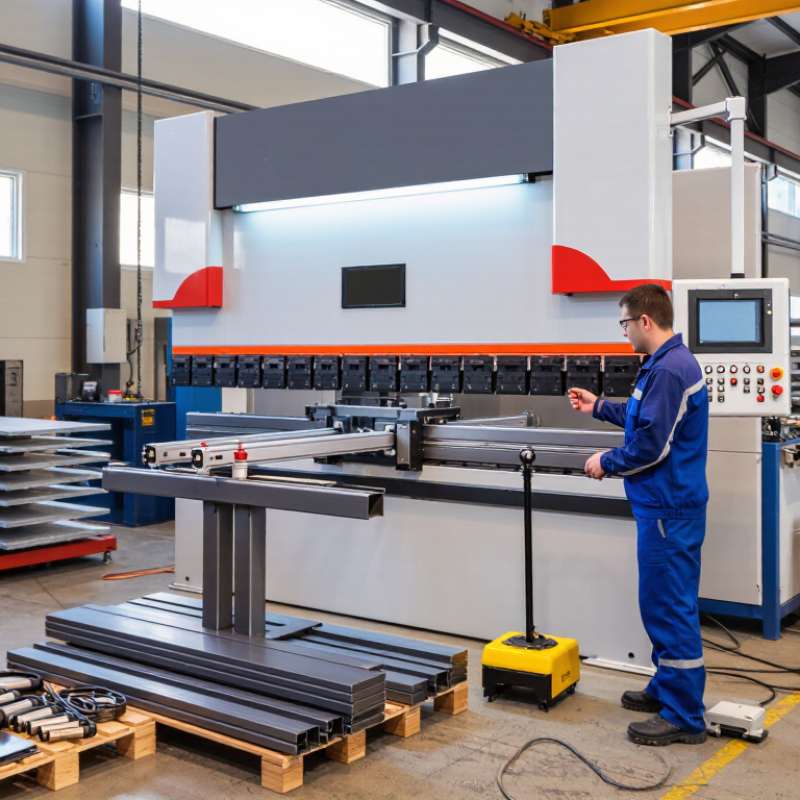
Pneumatic bending machines use compressed air to shape materials with controlled, repeatable force. Their clean operation suits workshops handling light sheet metal, aluminum parts, and thin stainless steel. Pneumatic press brakes work well for short flanges and simple boxes. Tube benders are better for railings, frames, and small fluid lines. Compact bench models fit repair stations where floor space matters. Choosing the wrong type creates uneven bends, wasted material, and frustration.

Check seven practical points before purchasing. Match the machine’s rated force with your material thickness and bend length. Confirm the available die shapes and punch sizes. Measure the required bend angle, stroke, and working height. Examine the air pressure and flow requirements carefully. A weak compressor can slow production. Inspect the control system, guarding, emergency stop, and foot pedal response. Ask about maintenance access and replacement seals. Small details matter.

During workshop trials, I measure the first five parts rather than trusting one successful bend. Springback can change with each alloy. I once underestimated this effect and had to adjust the tooling twice. That mistake was avoidable. Test the machine with your actual material, not only the supplier’s sample. Listen for air leaks. Watch the ram return. Check whether operators can load parts without awkward reaching. A lower purchase price may hide higher downtime. Capability should follow the application, not the other way around.

7 Tips for Choosing a Pneumatic Bending Machine? - Understanding Pneumatic Bending Machine Types and Applications

Tip Selection Dimension Machine Type or Configuration Typical and Useful Data Suitable Applications Important Limitation or Check
1 Define the workpiece geometry Sheet-metal press brake, tube bender, or profile bender Sheet-metal machines form flat blanks; tube and profile machines use dies matched to round, square, rectangular, or structural sections. Enclosures, brackets, ducts, handrails, frames, tubing, and light structural components A machine designed for sheet metal should not be assumed suitable for tube or profile bending without compatible tooling and work-holding.
2 Match force to material and thickness Pneumatic press brake or pneumatic forming press Required force depends on material strength, thickness, bend length, die opening, and bending method. Air pressure alone does not define bending capacity. Light-gauge aluminum, mild steel, stainless steel, and nonmetallic sheet forming when force requirements are moderate. Confirm the rated force curve, not only the maximum air pressure. Allow capacity for material variation and repeated production.
3 Choose the correct bending method Air bending, bottoming, or coining setup Air bending uses partial die contact and generally needs less force; bottoming improves angle consistency; coining requires substantially higher force. Air bending for flexible production; bottoming for repeatable angles; coining for specific high-force forming requirements. The tooling, machine force, springback allowance, and material must be evaluated together before selecting a process.
4 Check working length and throat depth Single-cylinder or two-cylinder pneumatic press brake The working length must exceed the bend line, while throat depth determines how far a part can extend behind the tooling. Larger machines may require greater air volume. Short brackets and panels with compact machines; long channels and cabinets with longer beds and deeper throats. Do not size the machine by sheet length alone. Include flange depth, side clearances, tooling width, and loading space.
5 Verify compressed-air requirements Pneumatic cylinder-driven bending machine Review operating pressure, air consumption per cycle, compressor flow, receiver capacity, filtration, and moisture control. Common industrial pneumatic systems often operate near 6 bar, but the machine specification governs. Workshops and production lines with stable, clean, dry compressed air. Insufficient flow can reduce speed and force. Pressure regulators, filters, lubricators where permitted, and drains should be maintained.
6 Evaluate accuracy, repeatability, and control Manual, foot-pedal, or programmable pneumatic control Mechanical stops, adjustable stroke, pressure regulation, position sensing, and programmable sequences can improve consistency. Actual accuracy depends on rigidity, tooling, material, and setup. Manual control for prototypes and low volume; programmable control for repeated batches and multi-bend parts. Request sample bend results using the intended material and tooling instead of relying only on a catalog accuracy figure.
7 Prioritize tooling, safety, and maintenance Interchangeable-die pneumatic bending system Useful features include guarded pinch points, emergency stops, two-hand or guarded controls, compatible punches and dies, replaceable seals, accessible air preparation, and documented maintenance intervals. Mixed production, job shops, educational workshops, repair work, and repetitive light-to-medium bending. Confirm compliance with applicable local machinery and workplace-safety requirements. Tooling availability and seal replacement support affect long-term operating cost.

Note: Performance ranges and suitability are indicative. Final machine selection should be based on the workpiece drawing, material specifications, tooling, production volume, compressed-air system, and applicable safety requirements.

Matching Machine Capacity With Materials, Thickness, and Bend Requirements

A pneumatic bending machine should be selected around the material, not only its advertised capacity. Mild steel, stainless steel, and aluminum require different force levels and tooling choices. A machine that bends thin aluminum smoothly may struggle with stainless steel of the same thickness. Check the rated capacity for your exact material and bend length.

Measure the sheet thickness with a caliper before ordering equipment. Then review the required bend angle, flange length, and inside radius. Short bends need less force than wide bends. Deep channels may also require more clearance than a simple 90-degree fold. Use the supplier’s force chart, but do not treat it as absolute. Actual results change with grain direction, surface condition, and tool wear.

Air pressure and cylinder size deserve close attention. Confirm that your workshop can provide stable pressure during repeated cycles. A pressure drop can produce uneven angles or incomplete bends. Test a sample using the intended tooling. That small trial often reveals problems that calculations miss. I have seen capacity estimates look acceptable, yet the finished flange still opened by several degrees. The lesson is uncomfortable but useful: leave a practical safety margin. Also inspect the frame, die opening, and back gauge adjustment. A powerful machine is not automatically a suitable one. The best choice matches thickness, material strength, bend width, production frequency, and the operator’s real working habits.

Checking Air Pressure, Force, Speed, and Precision Specifications

7 Tips for Choosing a Pneumatic Bending Machine

Checking Air Pressure, Force, Speed, and Precision Specifications

Start with the workshop’s actual air supply, not the machine’s ideal brochure figure. Measure pressure during production, when other tools may be running. A stable supply often matters more than a high peak rating. Check the required flow rate too. An undersized compressor can make each bend feel slow and inconsistent.

Match bending force to material thickness, width, and tensile strength. Leave practical capacity above your normal workload. This margin helps when harder batches appear unexpectedly. However, excessive force may waste energy and increase tool wear. Ask for force charts based on your actual metal, rather than relying on one impressive maximum value.

Speed needs careful interpretation. A fast approach stroke does not guarantee fast completed bends. Check return speed, setup time, and control response. Precision depends on frame rigidity, angle feedback, back-gauge repeatability, and tool alignment. Inspect sample bends with a calibrated angle gauge. I once trusted a displayed accuracy value and ignored material springback; the results were disappointing. That mistake still influences my inspections. Request repeatability data from several cycles, not one successful test. Listen for unstable valves, watch pressure changes, and confirm that operators can adjust settings safely. A clear service record also reveals whether the machine can remain dependable after months of daily use.

Evaluating Controls, Safety Features, Tooling, and Operating Convenience

Choosing a pneumatic bending machine requires more than checking its bending force. The controls should feel clear under pressure. Look for readable buttons, responsive foot pedals, and a simple pressure adjustment. Operators should change settings without reaching across moving parts. A confusing panel slows production and invites mistakes.

Safety deserves practical testing. Check the emergency stop, guarding, two-hand controls, and pressure-release system before purchase. Ask whether maintenance staff can inspect valves and hoses safely. Watch one complete bending cycle. Unexpected movement, delayed stopping, or excessive noise should raise concerns. I once saw a machine pass a quick demonstration but struggle with repeated cycles. That experience changed how I evaluate showroom claims.

Tooling determines accuracy. Confirm that dies match your common material thicknesses, bend angles, and part widths. Quick-change holders can reduce setup time, but only when they lock firmly. Examine the working height and loading space, too. Small ergonomic details matter during an eight-hour shift. Keep the gauge visible from the operator’s position. Confirm that replacement tools are easy to identify and store. Also, test the machine with your actual workpieces, not sample metal supplied by a seller. A spotless trial piece can hide setup difficulties. Convenience should include easy cleaning, accessible lubrication points, and clear service instructions. I would rather choose a slower machine with honest feedback than a fast model that leaves operators guessing.

Comparing Maintenance Needs, Energy Use, Warranty, and Total Cost

7 Tips for Choosing a Pneumatic Bending Machine?

Compare the machine’s five-year cost, not only its purchase price. Check maintenance access, spare-part availability, and required technician skills. Ask for a documented service schedule. Inspect valve blocks, seals, filters, hoses, and lubrication points. Small leaks matter.

The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks can waste 20–30% of compressor output.

Request measured air consumption at your actual pressure and cycle rate. Compare motor power, standby demand, and compressed-air use during partial loads. The Carbon Trust’s Compressed Air: Opportunities for Energy Savings report notes that compressed air can consume 10–15% of industrial electricity.

Price filters, seals, calibration, oil, and technician travel across five years. Review the warranty carefully. Confirm whether labor, pneumatic components, control systems, and emergency visits are included. A longer warranty is not automatically better. Response time may matter more.

Ask for written service targets and a list of exclusions. Compare expected downtime, setup time, and operator training requirements.

Include electricity, air generation, maintenance, and lost production in the total-cost calculation. Request test results, not optimistic estimates.

I would also challenge my own assumptions: a lower-energy machine may need expensive specialist service. Conversely, a simple design may use more air but remain easier to repair. Record real cycle data after installation, then revise the estimate.

Back to top