| 1. Verify the quality management system | Check whether the manufacturer has a documented quality management system and whether its scope covers the relevant production site and processes. | A current certificate, its scope and issuing body; or, if uncertified, documented procedures for process control, corrective action, and record keeping. | Does the certificate cover the facility making my parts? How are nonconforming parts identified, contained, and corrected? | ISO 9001 specifies requirements for quality management systems. Certification can support confidence in a system, but does not by itself guarantee that a specific part will meet its drawing. |
| 2. Match certifications to the application | Determine whether industry-specific requirements apply. For example, aerospace and automotive supply chains may require additional sector-specific quality systems. | Applicable certificates and scopes, customer-specific approvals where relevant, and a clear explanation of how requirements flow into production and inspection. | Which standards are required for this part or end market? Are these certifications current and applicable to the manufacturing location? | Certifications such as AS9100 for aviation, space, and defense organizations or IATF 16949 for automotive production are application-specific; they are not universal requirements for aluminum machining. |
| 3. Confirm material grade and traceability | Check that the proposed alloy, temper, product form, and applicable material specification match the drawing and service conditions. | Material test reports or certificates, supplier and lot identification, and a documented method for linking incoming material to finished parts. | Can each delivered lot be traced to its material documentation? How are substitutions approved and recorded? | Aluminum properties vary by alloy, temper, and product form. Specifications such as ASTM B209 for aluminum sheet and plate and ASTM B221 for extruded bars, rods, wire, profiles, and tubes cover different product forms. |
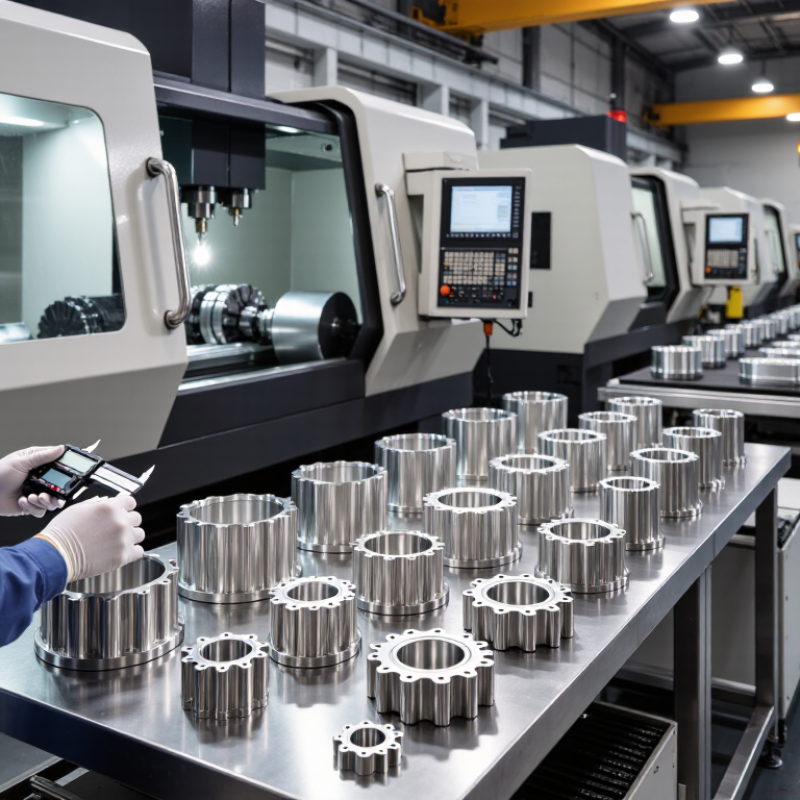
| 4. Review inspection equipment and methods | Confirm that inspection tools suit the feature being measured, including tolerances, geometry, surface finish, and measurement access. | A list of relevant instruments, calibration status, sample inspection records, and procedures for measuring critical drawing characteristics. | How are position, flatness, hole size, and surface finish measured? Can you show sample results for comparable features? | Micrometers, gauges, optical systems, and coordinate measuring machines (CMMs) serve different measurement needs. A CMM or other instrument should be selected based on the feature and required measurement capability. |
| 5. Examine calibration and measurement control | Look for a controlled calibration program, suitable measurement ranges, and records that connect equipment to recognized measurement standards where applicable. | Calibration records, equipment identification, due dates, and procedures for handling instruments found out of calibration. | How often is equipment calibrated, and what happens if a calibration check fails? Are measurement results recorded with the instrument used? | Reliable inspection depends on measurement equipment that is suitable and controlled. ISO/IEC 17025 concerns the competence of testing and calibration laboratories; it is not a general manufacturing certification. |
| 6. Assess process control and production capability | Review how machining parameters, setups, tooling, and process changes are controlled for the part’s critical dimensions and repeat production needs. | Process flow, control plans or inspection plans, first-article results when applicable, and examples of corrective action or process-change control. | Which features are considered critical? How do you monitor variation across a production run, and how are changes approved? | Repeatable process controls help maintain consistency between parts and production lots. Capability statistics are meaningful only when the process, measurement method, and data set are appropriate. |
| 7. Check final inspection, documentation, and delivery controls | Confirm that final checks cover drawing requirements, finishing or coating requirements, packaging, and required records. | Sample inspection report, nonconformance process, certificate of conformity if required, traceability records, and packaging or preservation instructions. | What inspection records accompany the shipment? How are surface damage, burrs, and handling risks controlled during packing and transport? | Clear acceptance records and suitable packaging help make deliveries easier to verify and protect precision surfaces and edges in transit. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS