| 1. Product Design and Application Fit |
| Gasket profile | Common metallic ring joint profiles include Type R, Type RX, and Type BX. | The profile must match the groove geometry, flange design, pressure class, and applicable piping or wellhead specification. | Dimensioned profile drawing, cross-section detail, and application guide. | Confirm profile compatibility |
| Standard reference | ASME B16.20 covers metallic gaskets for pipe flanges, while API 6A is commonly referenced for wellhead and Christmas-tree equipment. | The supplier should identify the governing standard and clearly separate standard dimensions from customer-specific requirements. | Standard reference list, technical datasheet, and compliance statement. | Check the latest applicable edition. |
| Nominal size and pressure class | Ring joint gaskets are manufactured for specific nominal pipe sizes and flange pressure ratings; dimensions are not interchangeable across all classes. | Design input should include nominal size, pressure class, flange or equipment drawing, groove dimensions, and operating conditions. | Approved drawing showing pitch diameter, ring width, height, and tolerances. | Match the gasket to the exact groove. |
| Operating temperature | Temperature capability depends on the selected alloy, process medium, pressure, and service environment. | Material selection should consider minimum and maximum operating temperature, thermal cycling, oxidation, and corrosion exposure. | Material recommendation and temperature-service assessment. | Review the complete pressure-temperature envelope. |
| Process medium | Oil, gas, steam, sour service, hydrogen-containing service, and corrosive chemicals may require different alloys and controls. | The ODM supplier should evaluate chemical compatibility, leakage risk, corrosion mechanisms, and any sour-service requirements before production. | Application questionnaire, material suitability statement, and technical review record. | State the medium and contaminants in the RFQ. |
| 2. Material Selection and Traceability |
| Typical material families | Carbon steel, stainless steel, duplex stainless steel, nickel alloys, and other corrosion-resistant alloys may be used depending on service. | The selected material must provide adequate strength, corrosion resistance, hardness control, and compatibility with the flange material. | Material comparison sheet and approved material specification. | Do not select material by temperature alone. |
| Material standards | Forged ring materials are commonly specified through ASTM or equivalent national and international material standards. | The purchase specification should define the material grade, heat-treatment condition, chemical limits, mechanical requirements, and acceptable substitutions. | Material test certificate with heat number and standard designation. | Verify the certificate against the order. |
| Sour-service requirements | Hydrogen sulfide service can require controls based on NACE MR0175/ISO 15156 or another project-specific sour-service specification. | Hardness, heat treatment, material chemistry, and environmental limits must be reviewed together rather than treated as separate checks. | Hardness report, heat-treatment record, and sour-service compliance declaration. | Confirm the exact project revision and service category. |
| Heat traceability | Metallic pressure-sealing components should be traceable to the original material heat whenever required by the purchase specification. | The heat number should remain linked from incoming material through machining, inspection, packing, and final documentation. | Heat-number log, material certificate, and product identification record. | Require traceability on the inspection plan. |
| 3. ODM Manufacturing Process |
| Engineering review | ODM production should begin with review of drawings, standards, tolerances, service conditions, and inspection requirements. | Conflicting requirements should be resolved before tooling, material purchasing, or batch production. | Contract review form, clarification log, and approved technical drawing. | Approve before production |
| Raw-material preparation | Forged or bar-stock material is selected according to the approved grade and manufacturing route. | Incoming material is checked for identification, dimensions, surface condition, and certificate consistency before machining. | Incoming inspection report and material certificate review. | Reject unidentified or mixed heat material. |
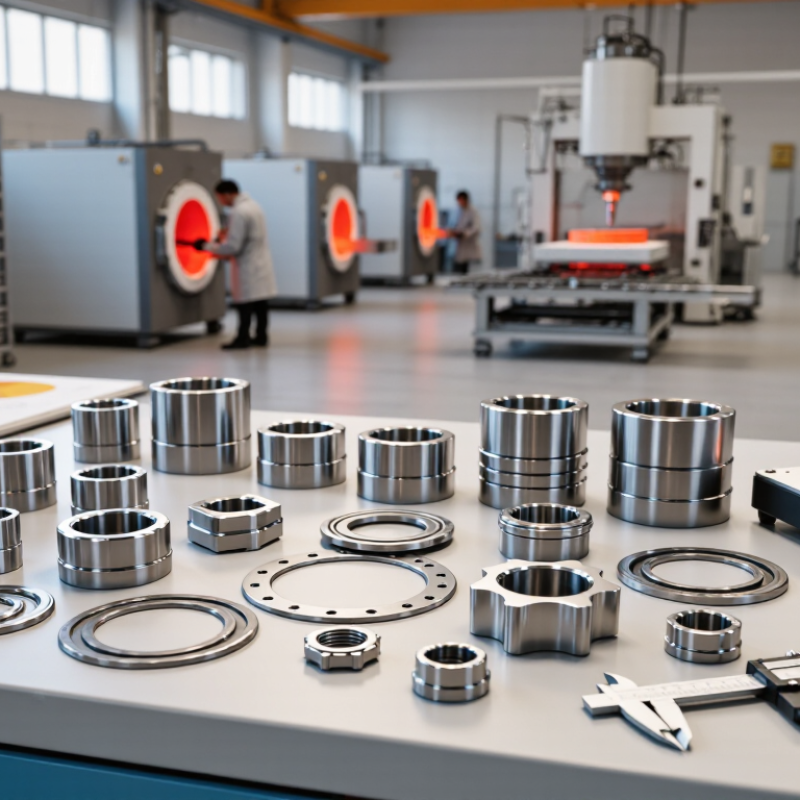
| Machining | CNC turning and precision machining are commonly used to produce the ring profile and sealing surfaces. | Machining programs should control groove-contact geometry, ring dimensions, surface finish, and edge condition. | Process route, CNC inspection record, and first-article report. | Review critical dimensions, not only overall diameter. |
| Heat treatment | Heat treatment may be required by the material specification or service requirement. | Temperature, holding time, cooling method, batch identity, and hardness results should be recorded where applicable. | Heat-treatment chart, furnace record, and hardness report. | Confirm that the treatment applies to the supplied heat. |
| Surface treatment and coating | Metallic ring joint gaskets may be supplied bare or with a specified coating, plating, or surface finish. | Any coating must be compatible with the operating medium, temperature, storage period, and flange-sealing function. | Coating specification, thickness record, and visual inspection report. | Specify whether coating is required or prohibited. |
| 4. Inspection and Quality Assurance |
| Dimensional inspection | Critical ring dimensions must be checked against the approved drawing and applicable standard. | Inspection should include pitch diameter, cross-sectional dimensions, height, width, ovality, and other project-defined characteristics. | Dimensional inspection report with calibrated instrument identification. | Require recorded values, not only a pass statement. |
| Surface condition | Sealing surfaces should be free from harmful cracks, laps, seams, dents, burrs, and unacceptable machining marks. | Visual inspection and, when specified, surface examination should be performed before final packing. | Visual inspection checklist and surface examination report. | Define acceptance criteria in the purchase order. |
| Non-destructive examination | Liquid penetrant, magnetic particle, ultrasonic, or other examinations may be required according to material and project risk. | The examination method must suit the alloy and detect the discontinuity types relevant to the component. | NDE procedure, examiner qualification record, and test report. | Specify method, coverage, and acceptance level. |
| Hardness verification | Hardness control is particularly important for sour-service applications and some project specifications. | Test location, method, frequency, and acceptance limit should be defined by the governing material or service specification. | Hardness map or batch hardness report. | Ensure the limit is project-specific. |
| Quality management | An ISO 9001-based quality management system is commonly used to control documented manufacturing processes. | The supplier should demonstrate control of nonconforming product, calibration, corrective action, document revision, and subcontracted processes. | Quality certificate, calibration list, corrective-action procedure, and audit records. | Verify certificate validity and scope. |
| 5. Packaging, Documentation, and Global Supply |
| Identification marking | Marking commonly includes size or profile information, material grade, heat or batch reference, and traceability code when required. | Markings must remain legible without damaging the sealing surface or creating an unacceptable stress concentration. | Marking photograph, packing list, and traceability register. | Approve marking format before shipment. |
| Packaging | Ring joint gaskets should be protected from impact, moisture, contamination, and corrosion during storage and transport. | Individual separation, protective wrapping, rigid cartons or crates, and desiccant may be used according to material and shipping conditions. | Packaging specification and pre-shipment photographs. | Prevent metal-to-metal damage during transit. |
| Export documentation | Typical documents include commercial invoice, packing list, certificate of origin where required, material certificates, and inspection records. | Document packages should use consistent part numbers, quantities, heat numbers, and revision references. | Sample document index and controlled final dossier. | Agree document requirements before order placement. |
| ODM sample approval | For a new design or modified profile, first-article approval reduces the risk of repeated production errors. | The supplier should submit a sample, drawing, inspection report, and material evidence before full-scale production. | First-article inspection report and signed approval record. | Use for new designs |
| Lead-time planning | Lead time depends on material availability, forging or bar-stock route, heat treatment, machining load, inspection scope, and documentation. | Suppliers should provide a milestone schedule rather than a single unqualified delivery date. | Production schedule covering material, machining, inspection, packing, and dispatch. | Separate standard items from custom ODM items. |
| Supplier comparison method | A qualified supplier should be evaluated on technical capability, traceability, inspection discipline, communication, and total delivered cost. | Use a weighted scorecard instead of selecting solely on unit price. | Completed supplier questionnaire, audit result, and quotation comparison. | Prioritize sealing reliability and documentation. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS